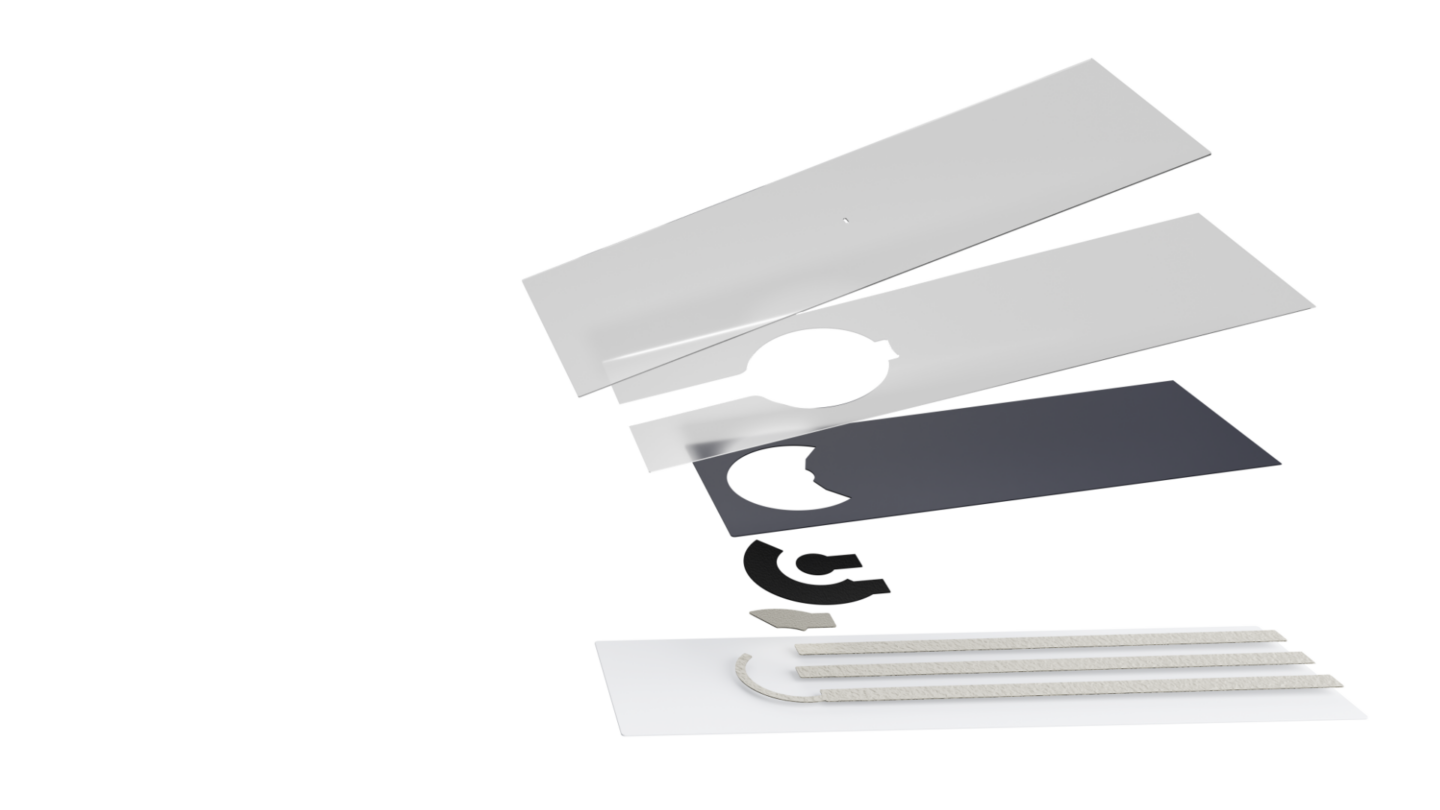
Electrochemical sensor manufacturing is the set of processes that turns conductive materials, insulating layers, and functional coatings into repeatable sensing devices. For disposable diagnostic sensors, the main stages are substrate selection, electrode layout design, screen printing of conductive and insulating inks, curing or drying, functional layer deposition, converting, inspection, and packaging. This guide focuses on how screen-printed electrodes are made, which materials and process controls determine repeatability, and what to consider when moving a design from prototype to production. For general sensing principles, sensor types, and applications, see the guide to electrochemical sensor types, principles, and applications.
What is the difference between electrode fabrication, functionalization, and device manufacturing?
Electrochemical sensor production is often described as a single process, but it consists of several distinct layers of work. Separating them clarifies who is responsible for what and where the main risks sit.
- Electrode fabrication covers printing and curing the conductive, reference, and insulating layers on a substrate. The result is a bare electrode structure with defined geometry and electrochemical behavior.
- Functionalization covers applying enzymes, antibodies, mediators, membranes, or other reagent layers to the working electrode. This step determines analyte specificity, and the chemistry itself is typically defined by the sensor developer.
- Electronics integration covers connecting the sensor to a reader, meter, or wearable electronics, including contact pads, connectors, and signal conditioning.
- Finished diagnostic device manufacturing covers assembling sensors into cartridges, strips, or housings, together with fluidics, labeling, and final packaging.
Each layer has its own process controls, quality requirements, and validation needs. Clarifying early which of these a project requires makes feasibility discussions and scale-up planning far more productive.
How are screen-printed electrochemical sensors manufactured?
Screen printing is the most widely used method for producing disposable electrochemical sensors in volume. It deposits conductive and functional inks through a patterned mesh onto flexible or rigid substrates. The process is fast, reproducible, and compatible with sheet-fed and roll-to-roll production, which is why it dominates single-use formats such as blood glucose strips and other point-of-care sensors.
A typical process sequence looks like this:
- Substrate preparation: The base film or sheet is cleaned, and where required pretreated, to ensure consistent ink adhesion and dimensional stability.
- Screen printing of electrode layers: Conductive inks, typically carbon or silver-based, are printed in successive layers to form the working, reference, and counter electrodes and their connection tracks. Each layer is dried or cured before the next is applied.
- Dielectric printing: An insulating layer is printed over the connection tracks, leaving only the active electrode areas and contact pads exposed. This defines the effective electrode area and therefore directly affects signal consistency.
- Functional layer application: Enzyme, reagent, or other biorecognition materials are deposited onto the working electrode, often by dispensing or printing under controlled conditions. Environmental control may be required to prevent contamination.
- Converting and singulation: Printed sheets are laminated with additional layers if required, then cut to final sensor geometry using mechanical or laser cutting.
- Inspection and testing: Electrical and functional testing confirms that sensors meet defined performance specifications before release.
- Packaging: Sensors are packaged, often under a controlled atmosphere, to protect functional layers from humidity and degradation during storage.
Other deposition methods, including inkjet printing, aerosol jet printing, and photolithography with thin-film metallization, are used where finer features or specific metals are needed. Screen printing remains the usual choice where cost per sensor and throughput matter most.
How do substrate and material choices affect manufacturing?
Material selection determines sensor sensitivity, selectivity, stability, and manufacturability. For medical applications, biocompatibility of all skin-contact or fluid-contact materials is an additional requirement.
Substrate materials
The substrate supports the electrode structure and must withstand printing, curing temperatures, and handling without distorting. Common substrates include polyethylene terephthalate (PET), polyimide, and paper for flexible or disposable sensors. Dimensional stability matters most: if a film shrinks or stretches during thermal curing, registration between printed layers suffers, which affects electrode area and alignment. Surface energy also influences ink wetting and adhesion, so pretreatment or substrate qualification is often part of process development.
Carbon-based electrode materials
Carbon inks, including carbon paste, graphite, and carbon black formulations, are widely used for working and counter electrodes because of their broad electrochemical window, low cost, and compatibility with screen printing. Their performance depends on the binder system, particle size and morphology, and curing profile. Because the electrochemical behavior of a printed carbon surface is sensitive to formulation and processing, switching ink batches or suppliers can change sensor response, and this needs to be managed through incoming material control and qualification.
Silver and silver/silver chloride systems
Silver inks serve as conductive tracks, and silver/silver chloride (Ag/AgCl) inks are the standard for reference electrodes, providing a stable, well-defined potential. The chloride content and layer thickness influence reference stability, particularly in samples or storage conditions that differ from those used during development.
Gold, platinum, and other materials
Gold and platinum are used in high-performance applications where surface chemistry control and low background noise are critical, though cost limits their use in disposable formats. They may be applied as printed inks or as thin films. Conductive polymers, nanomaterials, and mediator-modified inks are also used to improve signal amplification or surface area, but each adds process variables that must be controlled in production.
Dielectric inks
Dielectric inks define the exposed electrode area and protect the tracks. Their adhesion, curing behavior, and compatibility with downstream functional layers and sample liquids all influence sensor reliability.
What are the critical process considerations for repeatable production?
Repeatability is the central manufacturing challenge for electrochemical sensors. Small variations in layer thickness, edge definition, or surface condition translate directly into variation in measured current or potential. The main areas of control include:
- Printed layer properties: Thickness, resistivity, and surface morphology depend on ink rheology, mesh specification, squeegee parameters, and curing conditions.
- Pattern accuracy and registration: Electrode area is often defined by the dielectric opening, so print-to-print registration and edge definition influence active area and signal consistency.
- Curing and drying: Temperature, time, and airflow affect residual solvent, binder crosslinking, and electrode surface behavior. Incomplete or inconsistent curing is a common source of drift.
- Contamination control: Particles, residues, and handling contamination can alter electrode surfaces. Controls are especially important before functional layer deposition.
- Material repeatability: Ink batch variation, substrate lot variation, and storage conditions of inks and reagents all affect output.
- Process stability over time: Ink viscosity changes during long print runs, and screens wear, so in-process monitoring and defined intervention limits are needed.
Manufacturing stages, critical considerations, and failure mechanisms
The table below summarizes the main stages of screen-printed electrochemical sensor manufacturing. It reflects general industry practice rather than the specification of any single product.
| Process stage | Purpose | Critical considerations | Potential failure mechanisms |
|---|---|---|---|
| Substrate preparation | Provide a clean, stable surface for printing | Surface energy, cleanliness, dimensional stability, storage conditions | Poor ink adhesion, layer misregistration, delamination |
| Conductive layer printing | Form electrodes and connection tracks | Ink rheology, mesh and squeegee settings, layer thickness, registration | Thickness variation, resistivity drift, pinholes, track breaks |
| Reference electrode printing (Ag/AgCl) | Provide a stable potential baseline | Chloride content, layer thickness, curing profile | Unstable or drifting reference potential |
| Curing or drying | Remove solvent and set the ink structure | Temperature, time, airflow, substrate shrinkage | Residual solvent, cracking, inconsistent electrode behavior, warping |
| Dielectric printing | Insulate tracks and define active electrode area | Opening accuracy, edge definition, adhesion, coverage | Variable electrode area, leakage paths, sample ingress under the insulation |
| Functional layer deposition | Apply the recognition or reagent layer to the working electrode | Deposition volume and position, environmental control, reagent handling | Inconsistent coverage, contamination, loss of activity |
| Converting and singulation | Laminate and cut sensors to final geometry | Cutting accuracy, lamination alignment, handling damage | Edge damage, contact pad contamination, misaligned layers |
| Inspection and testing | Verify visual, electrical, and functional performance | Defined acceptance criteria, sampling plan, measurement repeatability | Defects escaping detection, inconsistent test conditions |
| Packaging | Protect sensors during storage and shipment | Humidity and oxygen control, desiccation, seal integrity | Reagent degradation, shelf-life loss, moisture-related drift |
How is electrode performance characterized and tested?
Electrochemical characterization confirms that printed electrodes behave as intended before and after functionalization. Common approaches include cyclic voltammetry with a well-behaved redox probe to assess electroactive area and electron transfer behavior, electrochemical impedance spectroscopy to evaluate interface properties, and chronoamperometry to check response consistency. Physical checks, such as layer thickness, sheet resistance, and visual or optical inspection of print quality, complement these measurements.
Test methods should be defined during development, because acceptance limits set at this stage become the basis for production inspection. Characterization performed on bare electrodes also helps separate problems in electrode fabrication from problems in functionalization, which speeds up root-cause analysis. Screentec operates an ISO 5 white room for electrochemical characterization and small-scale biofunctionalization, supporting customers who require this level of environmental control during sensor development and early manufacturing.
What does it take to move from prototype to production?
Scaling an electrochemical sensor from laboratory prototypes to repeatable production involves more than printing larger quantities. Typical considerations include:
- Design for manufacturability review: Electrode geometry, track widths, spacing, and registration tolerances should be checked against what the printing process can reliably hold.
- Material qualification: Inks, substrates, and reagents need to be qualified, with incoming controls and defined handling and storage requirements.
- Process definition and transfer: Print parameters, curing profiles, and handling steps are documented so that they can be reproduced across runs and operators.
- Inspection strategy: In-process checks and final release tests are defined, with acceptance criteria linked to sensor performance requirements.
- Process validation: For medical devices, the process is typically validated to show that it consistently produces product meeting specification, supported by documentation and traceability appropriate to the applicable quality system.
- Capacity planning: Sheet-fed and roll-to-roll options differ in throughput, setup effort, and suitability for different volumes.
Regulatory strategy, clinical validation, and product approval remain the responsibility of the device developer, but a manufacturing partner’s documentation and process control can support those activities.
How do early design decisions affect manufacturability?
Many production problems originate in decisions made during prototyping. Electrode geometry that is acceptable for hand-made prototypes may be impossible to print consistently at volume. A functionalization method that works on the bench may not translate to controlled, high-throughput deposition. Choosing an ink or substrate for its laboratory performance without checking supply continuity, batch variability, or curing compatibility can force redesign later.
Practical steps that reduce risk include evaluating geometry and material choices against both electrochemical performance and printability at the same time, specifying tolerances that reflect real process capability, and involving manufacturing expertise during feasibility or early prototype stages rather than after design freeze.
Where does this fit in diagnostic device development?
Screen-printed electrochemical sensors form the detection element of many in vitro diagnostics products, from test strips to microfluidic cartridges. Screentec supports customer-defined electrode, sensor, and diagnostic manufacturing projects; the sensor design, assay chemistry, and regulatory pathway remain with the customer. More information on production capabilities is available on the production services page.
If you are planning a screen-printed electrode or electrochemical sensor project and want to assess manufacturing feasibility, material options, or production scale-up, discuss your custom screen-printed electrode manufacturing project with Screentec.
Frequently Asked Questions
What materials are most common in screen-printed electrode manufacturing?
Carbon-based inks are the most common choice for working and counter electrodes, silver and silver/silver chloride inks are used for conductive tracks and reference electrodes, and dielectric inks provide insulation. Gold and platinum are used where higher performance justifies the cost. Substrates are typically PET or polyimide films, with paper used in some disposable formats.
How is electrode geometry optimized with manufacturing in mind?
Electrode geometry affects signal magnitude, mass transport of the analyte, and the ratio of signal to background noise. Optimization typically involves iterative fabrication and electrochemical characterization of different geometries, evaluated against printing tolerances and yield at the same time. Decisions made here have direct consequences for printability and repeatability in volume manufacturing.
What are the most common mistakes when transitioning an electrochemical sensor from prototype to production?
The most frequent mistake is locking in material and process choices during prototyping without evaluating their manufacturability at scale. Other common pitfalls include underestimating ink or substrate batch variability and delaying engagement with a manufacturing partner until after design freeze, when redesigns are costly. Involving manufacturing expertise early significantly reduces these risks.
How is sensor selectivity validated against real sample matrices?
Selectivity validation should use samples that closely replicate the intended matrix, such as whole blood, sweat, or food extracts. Known concentrations of common interferents are spiked into the matrix, and the sensor response is compared with the response to the target analyte. Regulatory submissions typically require this data in a structured format, so building interferent testing into the development plan from the start avoids gaps later.
What does ISO 13485 require from a sensor manufacturer, and why does it matter?
ISO 13485 requires a documented quality management system covering design controls, supplier qualification, process validation, traceability, and corrective action, tailored to medical device production. For device manufacturers sourcing sensor components, working with a supplier operating under such a system provides documented evidence that components were produced under controlled conditions, which auditors and notified bodies expect to see.
How can shelf life and stability be addressed for disposable biosensors with enzyme-based recognition elements?
Enzyme stability is primarily managed through immobilization chemistry, stabilizing additives, and controlled packaging conditions such as desiccation and inert atmosphere sealing. Accelerated aging studies at elevated temperatures help predict real-time shelf life and identify formulation weaknesses early. Stability should be tested under the full range of conditions the product will encounter during storage and shipping, not only ideal laboratory conditions.
Does electrode fabrication include biosensor functionalization?
Not necessarily. Electrode fabrication produces the printed electrode structure, while functionalization adds the recognition layer, such as an enzyme or antibody, to the working electrode. The two are separate steps with different controls, and responsibility for the chemistry typically rests with the sensor developer.